When a busbar comes off the line with a defect, the real question is whether the part can be restored to specification or must be scrapped. This guide sets out the rework and repair acceptance rules: eligible defects, hard scrap conditions, the dimensional, plating, insulation and mechanical checks after repair, the traceability record, and when the customer must be notified and files updated.
When a busbar comes off the line with a defect, the real question is whether the part can be restored to specification or must be scrapped. This guide sets out the rework and repair acceptance rules: eligible defects, hard scrap conditions, the dimensional, plating, insulation and mechanical checks after repair, the traceability record, and when the customer must be notified and files updated.
A busbar that arrives at inspection with a defect usually has three possible dispositions: it may be accepted as-is under a documented concession, it may be reworked and sent back through reinspection, or it may be scrapped. This guide deals only with the second path — the acceptance and rejection rules that apply after a busbar has already been reworked or repaired inside production. It does not cover diagnosing faults that appear after the bar has been installed in a cabinet, inverter or battery rack; that field-maintenance work follows a separate maintenance and service procedure.
The three terms are easy to blur on the shop floor, and separating them at the outset decides who can sign the part off. Rework is action taken on a nonconforming product so that it meets the original drawing, purchase specification and acceptance standard again. Repair is action that restores the part to a usable condition but leaves it, in some respect, not identical to the original specification; a repair therefore usually needs a documented deviation or concession before shipment. Concession is the recorded approval to release product that still departs from the drawing, and whether your supplier can grant it unilaterally or must obtain your signature depends on the contract and the customer-approved quality plan.
The acceptance logic in this guide applies across stamped, bent, laminated and insulated copper busbars, as well as copper links, posts and straps assembled with studs, crimped terminals or welded joints. The actual pass/fail values for thickness, section, insulation level, torque and pull-off are not repeated here; every such number is set by the project drawing, the purchase specification and the agreed acceptance standard, and must be read from those documents before the first rework decision is made.
Read this document alongside the broader inspection practice covered in our quality and acceptance record page, which describes how inspection evidence is collected, stored and handed to the customer. If your drawings have not yet been released to manufacturing, the busbar design guide shows where acceptance requirements should already have been written down.
Before anyone touches the defective part, it enters a controlled review. The bar — together with its serial or batch identification, its traveler and the inspection records that flagged the defect — is tagged as held, segregated from conforming stock, and kept in a place where it cannot be packed or shipped by mistake. Mixing held parts with released stock is how a rejected busbar leaves the plant, and no amount of later paperwork fixes that.
The review first records where the defect was found. It may have appeared at an in-process station after bending, punching, plating or lamination; at final inspection after all operations; or in a returned lot from the customer or the next assembly stage. The origin matters because it points at which process step should be corrected, and it changes how much of the lot must be examined for the same problem. A defect that appears only on one terminal of one part may be isolated; a defect that traces to a plating bath, a crimp tool or a laminate roll can affect a whole batch and triggers a broader look-back.
Evidence is captured before rework begins: the location and character of the defect, the dimensions measured against the drawing, any surface or insulation condition, and the readings from prior inspection. Photographs or scans of the affected area are kept with the record. At this stage quality engineering owns the disposition decision; structural, electrical or thermal-risk questions go to product engineering; anything that touches a customer-approved specification goes through the customer-notification route described later in this guide.
Not every defect can be repaired, and the first cut at eligibility follows one principle: the repair must restore the part to a condition that can be verified against the original specification, without changing its load-carrying geometry, its dielectric system or its thermal history in a way the drawing does not permit. The following classes of defect are the ones that shops commonly treat as reworkable, provided the base conductor and the joint under the defect remain sound:
Each of these entries is only a candidate. Eligibility still depends on the position of the defect (contact zone, bend zone, field-stress edge or plain body), on whether the defect reaches a critical dimension, and on what the acceptance standard allows. A touch-up that would be acceptable on an outer body edge may be rejected on a mating terminal face.
Some conditions cannot be made good again by rework, because the damage is internal, structural or thermal rather than a surface or assembly mistake. The shop floor should treat the following as scrap conditions unless a qualified engineer and, where required, the customer issue a written deviation; reworking past these lines tends to produce a part that looks repaired but carries the original failure mode into service:
When a defect sits near one of these scrap lines, the default decision should be conservative. Escalation to engineering and the customer costs time; shipping a part that carries an unknown residual risk costs far more, and a rework that hides an overheated joint or a delaminated layer tends to reappear as a field failure under load.
The table below condenses the rework decision into four columns you can use at the inspection bench: the defect type, whether it is reworkable or must be scrapped, the checks that must be repeated after any accepted rework, and what the record must contain. Numeric limits are intentionally left out of the table; they come from the drawing, the purchase specification and the agreed acceptance standard for the project.
| Defect type | Disposition | Mandatory post-rework checks | Record requirements |
|---|---|---|---|
| Loose or under-crimped terminal; damaged or wrong stud | Reworkable: re-crimp or replace stud with approved hardware | Terminal and hole dimensions, torque and pull-off check, contact-surface visual, joint position against drawing | Operator, terminal/stud hardware lot, rework method, torque and pull-off readings, inspector identity and date |
| Small local plating scuff or missing finish on a non-contact edge | Reworkable by local touch-up or re-plating, base metal intact | Plating thickness and adhesion per spec, edge covering, visual blend, absence of exposed copper in touched zone | Zone touched, bath or material lot, thickness and adhesion readings, inspector and date |
| Damaged insulation film, sleeve or coating; copper undamaged | Reworkable: replace insulation with approved material | Insulation resistance, withstand/hi-pot, creepage and clearance, fit and coverage, marking visibility | Insulation material lot, replacement description, dielectric and resistance readings, inspector and date |
| Mild warpage or out-of-flatness, no crack or section loss | Reworkable: controlled leveling or straightening | Flatness, overall dimensions and hole position, bend radius and temper condition, mating fit | Leveling method, flatness reading, dimensional results, inspector and date |
| Wrong, missing or illegible marking | Reworkable: correct or re-apply mark | Legibility, mark location per drawing, traceability code, no conflicting old mark remains | Old mark disposition, new mark applied, inspector and date |
| Dielectric delamination or through crack in laminated stack | Scrap — do not rework | None on the repaired path; record rejection evidence instead | Serial/batch, defect description and evidence, scrap reason, disposition authorization |
| Large-area plating loss with exposed base metal beyond touch-up zone | Scrap, unless a full re-finish is spec-approved or a customer concession is granted | Where concession is pursued: plating thickness, adhesion and covering on the whole bar | Inspection evidence, drawing/spec reference, concession holder and approval level, inspector and date |
| Conductor section thinning or machining damage beyond allowed allowance | Scrap | None on the repaired path; measurement retained as rejection evidence | Measured condition, drawing section reference, scrap authorization, inspector and date |
| Previously overheated terminal or joint zone (discoloration, softening, insulation damage) | Scrap — replating or retightening does not restore properties | None on the repaired path; thermal or condition evidence retained | Observed condition, available thermal history if any, scrap reason, authorization, inspector and date |
Read the "mandatory checks" column as a minimum set. Some of these checks overlap with first-article inspection: after a rework that changes a joint, a plated surface or an insulation system, the affected family of tests is repeated even if other families were untouched.
A rework is accepted not because the repair was done neatly, but because it was done with the same materials, process controls and acceptance criteria as the original build. Ad-hoc bench fixes — a dab of solder where the spec calls for a crimp, a wrap of generic tape where a qualified film belongs, a hand file to chase a hole — are repairs in name only, and they carry the risk the original process was designed to avoid.
Terminal and stud work. A defective crimp is remade with the approved terminal, the correct tooling and the same crimp parameters documented for the original joint. A damaged stud is replaced with hardware from the approved lot; if the threaded or weld interface itself is damaged, the part moves toward scrap rather than a swap. The rebuilt joint is then treated as a new mechanical joint for inspection.
Local re-finishing. A local touch-up follows the plating and surface-finish sequence the finish specification allows: surface preparation, deposition or re-tinning within the qualified process, and any post-treatment such as anti-tarnish protection. Where the defect reaches a contact face or a high-field edge, the question of whether local repair is allowed goes to engineering rather than being decided at the bench. Our electroplating process guide explains how coating deposition, masking and edge finish are normally controlled in production; the rework route should follow the same controls rather than improvise around them.
Insulation replacement. A damaged insulator is replaced with the material and thickness specified on the drawing; substituting a locally available sleeve or tape changes the dielectric system and needs engineering approval. Leveling. Straightening is done with controlled force and checked for spring-back, with attention to whether the bend zone has been worked. Marking. The old mark is removed or covered in an approved way so it cannot be read alongside the new one.
For a one-off replacement bar built to a customer drawing, the same material and finish controls apply. Replacement custom copper busbars listed on the product page carry a sample price from US$47 on the product page; series pricing is quoted per drawing, and any rework on those bars follows the inspection record path in this guide rather than a separate shortcut.
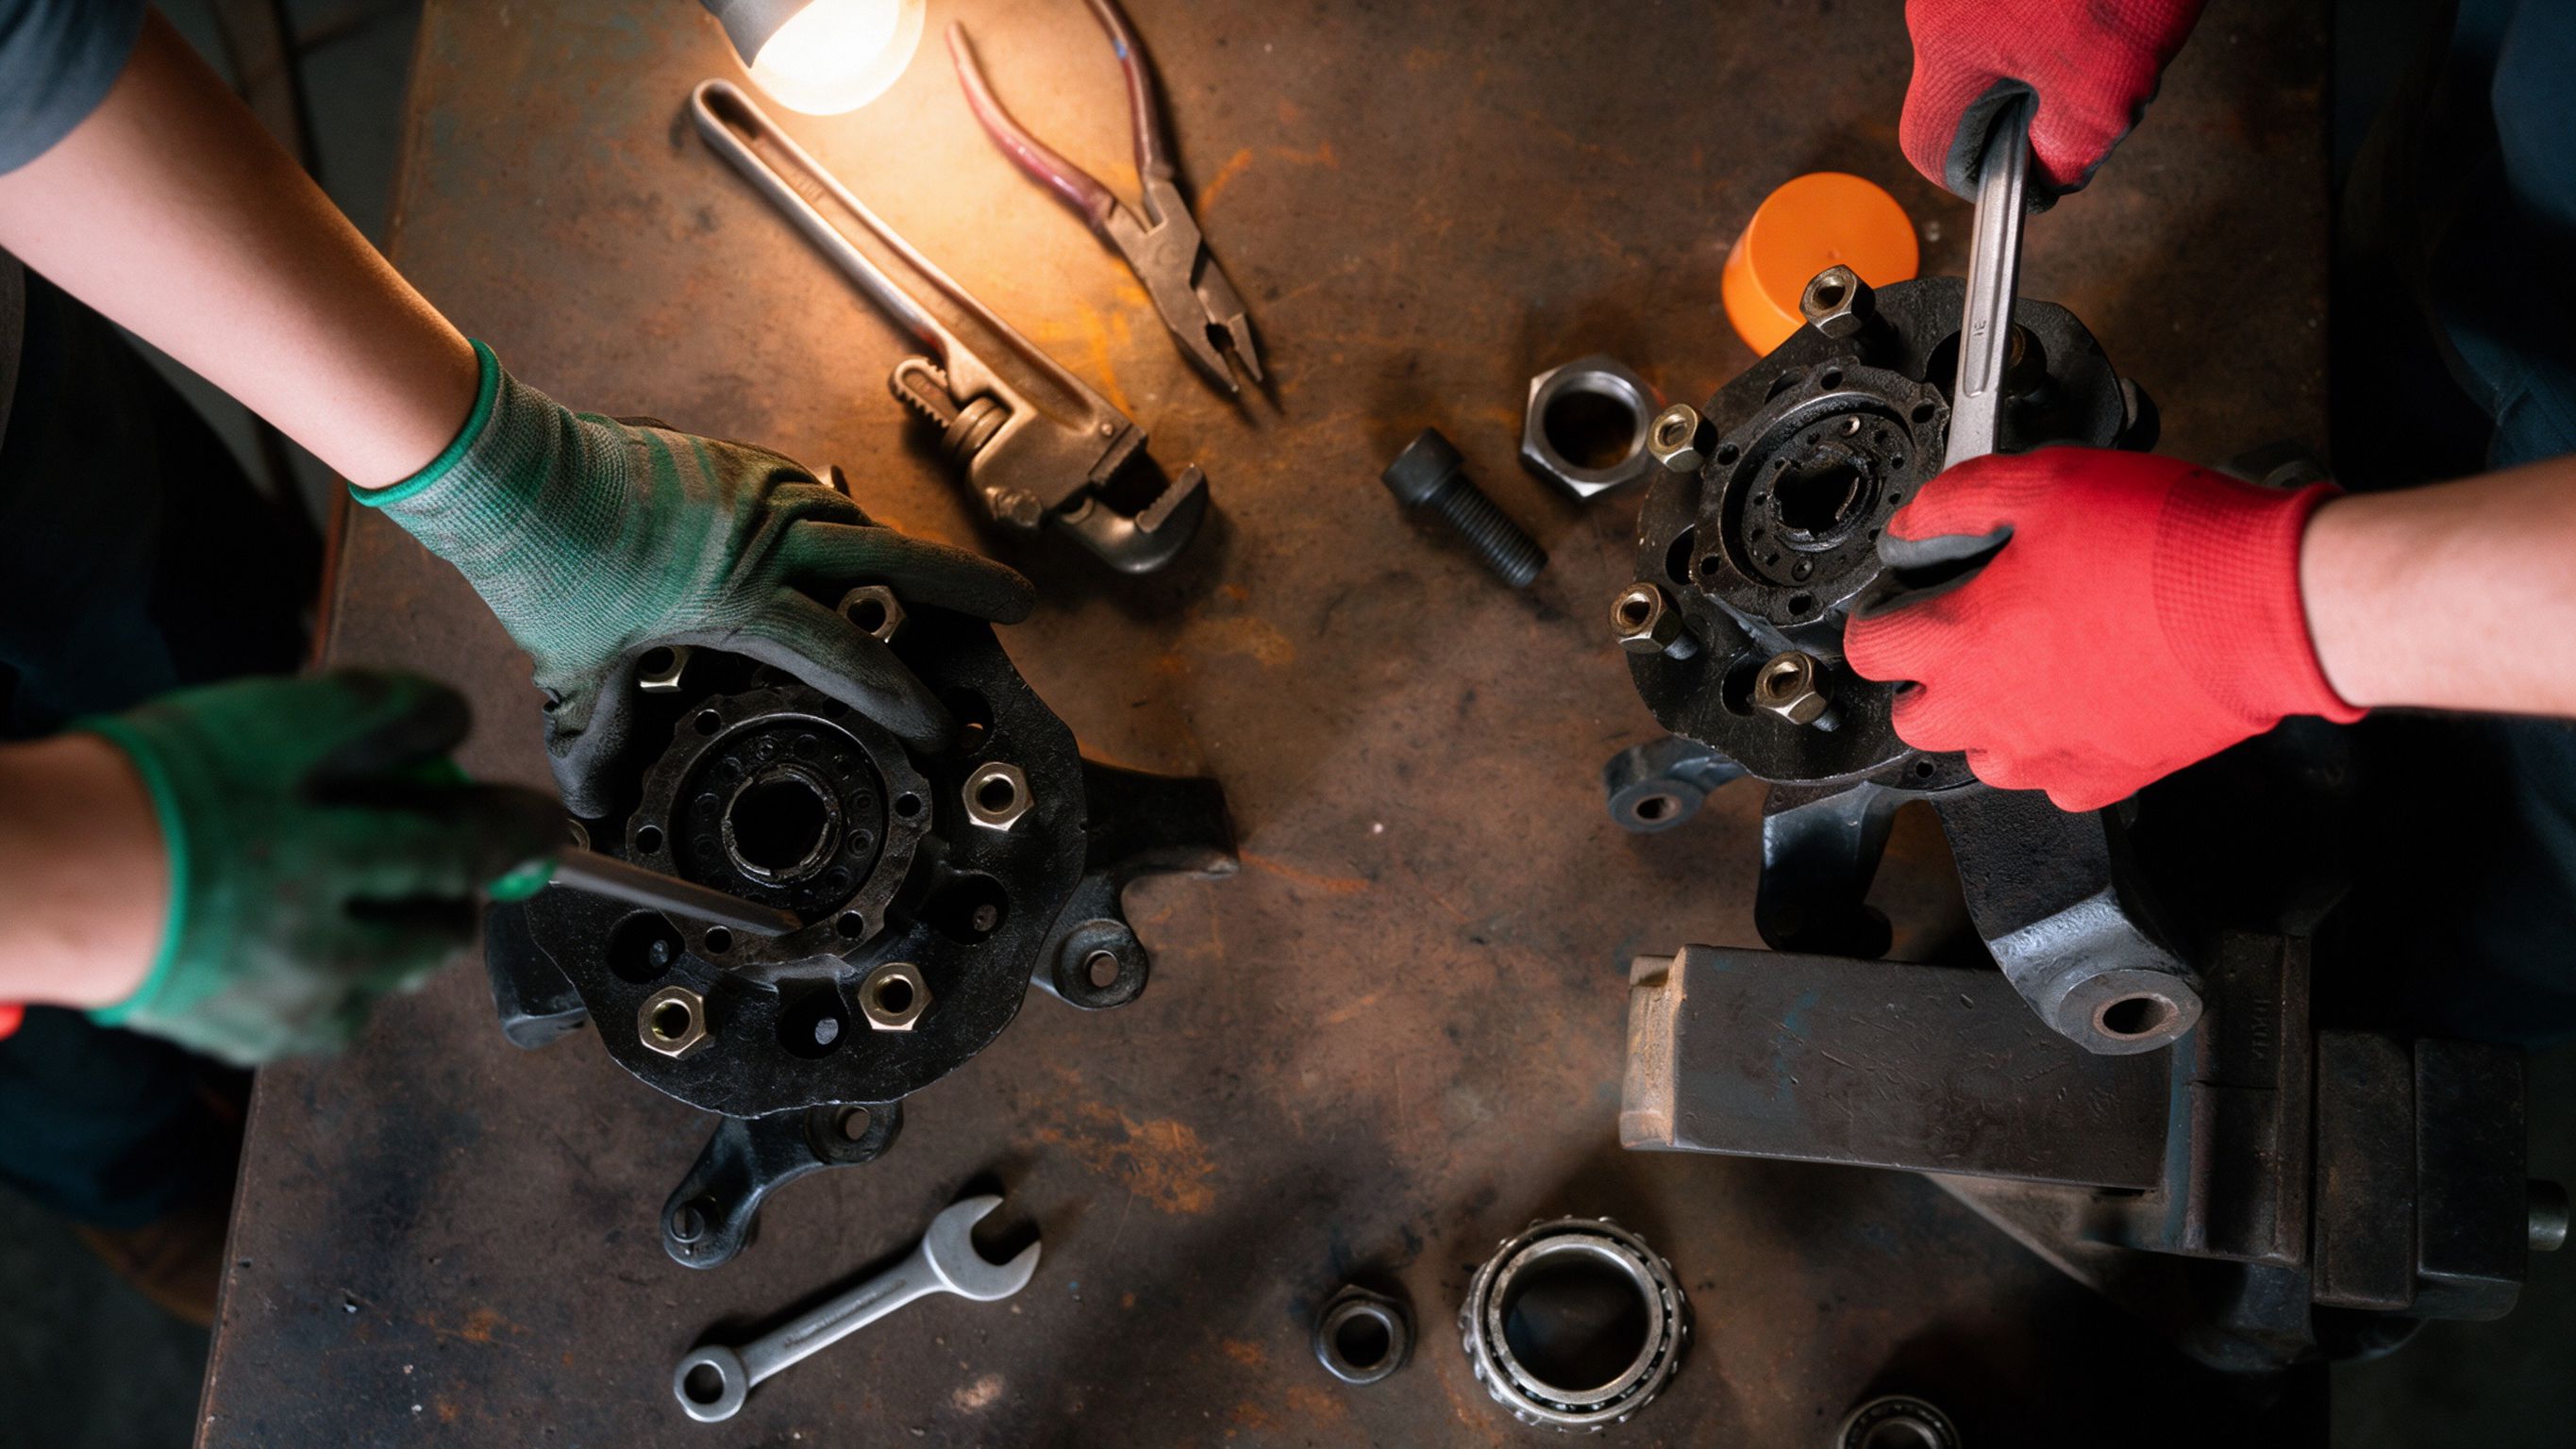
After any rework that touched the body, a terminal, a bend or a hole, the bar goes back through dimensional inspection against the released drawing. The inspector checks overall length and width, hole positions and diameters, terminal spacing, bend angles and bend radii, and any datum dimensions that the mating assembly depends on. Where the rework involved leveling, flatness is measured over the specified reference surface and compared with the drawing tolerance; a bar that sits flat on the bench but rocks against its mounting faces has not actually been leveled.
Fit checks matter as much as single measurements. A reworked terminal that re-crimped cleanly still has to line up with its mating stud or lug; a replaced insulation section still has to clear the adjacent parts in the stack. Where possible, the bar is dry-fit against a mating fixture or an assembly mock-up before release, and the fit observation is recorded alongside the dimensional readings.
The dimensional record captures the measured values, the gauge or method used, and the inspector. Dimensions that were not affected by the rework do not all need to be re-measured, but the record should say which dimensions were rechecked and why the rest were left alone. This distinction keeps the reinspection proportional: a remade terminal does not require re-measuring every plain body dimension, but it does require checking every dimension the joint touches.
Where rework touched the surface finish, the reinspection verifies that the replacement finish meets the specification on thickness, adhesion and covering, rather than judging it by appearance alone. Thickness is checked at the touched zone and at the transition into the original finish; adhesion is assessed by the method the acceptance standard defines; covering is inspected to confirm there are no skips, exposed base metal or porous patches along edges and holes.
Local touch-ups are the places where finish quality tends to differ most from the original bath-deposited surface. The blend around the repaired zone is checked for rough edges, buildup at the boundary and any corrosion risk where the new finish meets the old. If the touched zone is a mating contact surface, the finish condition there is treated under the contact-zone requirements of the specification rather than the looser rules that apply to non-contact edges.
Any re-finish that had to remove original plating to reach sound base metal is reviewed against the section-thinning scrap rule in Section 4. If the repair process itself removed material beyond the allowed allowance, the finish looks recovered but the conductor section has already crossed the scrap line. Surface-finish selection and the trade-offs between tin, silver and protected copper are covered in the finish-selection material on this site; the rework decision should reference the finish actually specified on the drawing, not the preferred finish for a new design.
After an insulation replacement, a re-coated section or any rework near a live-to-nearby-metal boundary, the dielectric performance of the repaired zone is retested before the bar is released. The reinspection follows the insulation test sequence the project specification defines: insulation resistance across the relevant surfaces, a withstand or hi-pot check between conductor and grounded structure, and verification that creepage and clearance distances at the repaired edge still satisfy the insulation-coordination requirements for the voltage level.
For laminated bars, a repair that opened the stack or replaced a film deserves extra care: the layer order, the film overlap at edges and the absence of entrapped air or adhesive gaps are checked visually and, where the project calls for it, with internal inspection. Internal voids and delaminations do not reveal themselves on a routine withstand test, which is why a laminated bar that has been opened and restacked is reviewed against the same internal-information expectations as a new build. Our insulation testing guide describes the resistance and withstand checks in more detail, and the void and CT inspection guide explains when internal imaging is needed to confirm layer integrity.
A repaired insulation that passes a withstand test at room condition still has to cover the service environment: humidity, contamination, temperature cycling and vibration can all age a repaired seal faster than the original factory bond. Where the application is outdoor, humid or chemically exposed, the engineering review should confirm the replacement material and the repair method match that environment rather than the cleaner bench conditions under which the test was run.
Every reworked or replaced mechanical joint is revalidated as a joint, not accepted because the fastener looks seated. The check follows the joint type: threaded studs and bolted terminals go through the specified torque sequence, crimped or welded terminals are checked for mechanical retention, and any joint that depends on contact pressure is verified to carry load the way the original design intended. Pull-off or retention testing, where the specification calls for it, is performed on the rebuilt joint and recorded rather than inferred from the original joint's test history.
Joint performance after rework depends on surface condition as much as on the fastener: a mating face that was scratched, re-tinned or touched up during the repair can change contact resistance and relaxation behavior. The contact zone is inspected for damage, and if the rework altered the interface material, the joint may need the contact-performance review the original qualification covered. The terminal torque and pull-off acceptance guide sets out how these joint checks are documented and what the acceptance record should contain.
Mechanical reinspection also covers what the rework may have disturbed indirectly: a leveling operation can shift a stud or a hole; a local re-finish can leave residue on an insulating washer or a thread; a replaced insulator can change how the joint clamps down. The inspector walks the bar for secondary effects rather than checking only the repaired spot.
A reworked part is traceable only if the record lets someone later answer, in plain terms, what was wrong, what was done, what materials went in, who checked it, and what the results were. The record travels with the part through the remainder of production and stays with the batch documentation on release. A record that says simply "reworked and passed" cannot support an audit, a customer complaint review or a later field investigation.
The minimum record contents are:
Where the same defect recurs across several parts, the record also feeds the corrective-action loop: the rework entries are grouped by defect type and process step so the root cause in fabrication can be addressed instead of repairing parts one at a time. A shop that spends its effort repairing repeat defects without fixing the upstream process will accumulate rework cost and risk faster than it improves quality.
Not every internal rework reaches the customer, but the line between internal rework and customer-facing deviation is defined by the contract, the approved quality plan and whether the part still matches its released specification. The default rule is conservative: if the action restored the part to the original spec by an approved rework method, it can usually stay internal; if the part was repaired rather than reworked, or if the rework touched a feature the customer approved at first article, the customer is notified before release.
Customer notification is required at least in these situations: the repair leaves a deviation from the drawing or purchase specification; the rework changes a material, finish or joint type that was part of the approved build; the affected part belongs to a customer-approved first-article or qualification lot; or the rework follows a defect that also affected already-shipped units and requires a look-back. The notification should carry the same information as the internal record: what happened, what was done, what was rechecked, and the evidence behind the disposition. Whether the customer signs the concession, accepts a rework confirmation, or asks for a full retest is decided case by case, but the decision should be on paper before the part ships.
Files are updated to match the as-built condition. Drawing or specification references on the traveler reflect the actual revision used; the quality record shows the rework and reinspection; any concession is filed with the lot. If the rework reveals a recurring design or manufacturing weakness, the change feeds back into drawing or process revision rather than being absorbed into a single repaired part. The qualification logic after a material or process change mirrors what our second-source requalification guide describes: a change that affects a joint, finish or insulation system can require repeating the relevant qualification checks, not just the bench inspection on the repaired bar.
If your project has special acceptance obligations, audit evidence requirements or a contract that names a concession process, raise the case with our engineering and quality team through the contact page before the rework is closed, so the right approval level and file update are in place rather than reconstructed afterward.
A consistent rework acceptance routine runs the same order every time: hold and segregate, record the defect and evidence, judge eligibility against the scrap and rework rules, perform the rework inside the qualified process, run the mandatory reinspection families, write the traceable record, and then decide whether customer notification or a file update is required. Skipping the record step to save time, or deciding eligibility after the repair has already started, are the two habits that most often turn a contained defect into a shipped problem.
Escalation should be triggered early when the defect sits near a scrap line, touches a contact or high-field zone, involves an overheated or annealed area, or affects a customer-approved feature. Quality engineering and product engineering review together; the customer is brought in before release wherever the contract calls for it. When a batch shows the same defect more than once, the escalation moves from part-level disposition to a process-level corrective action.
When you review a supplier's rework practice, ask what their disposition categories are, how they separate rework from repair and concession, which inspections repeat after each repair type, how the rework record is linked to the serial or lot, and which situations require customer sign-off. A supplier who can show the record format, the check list and the approval route is further along than one who describes rework as "we fix it and check it over." For the upstream side of the same quality gate, the drawing release DFM checklist shows how acceptance requirements should be fixed on the drawing before production starts, so fewer defects reach the rework stage in the first place.
One boundary is worth stating plainly: after a thermal event in a battery or power installation, damaged busbars and interconnects are judged under the event's own safety and replacement rules, not under a shop-floor repair logic. The BESS fire code enforcement guide covers what inspectors and code bodies expect from replacement and residue documentation in that context; this guide's rework and scrap rules apply to production nonconformities, not to post-event field hardware.

A second source is supposed to reduce risk, and it usually adds some instead: the drawing
Read article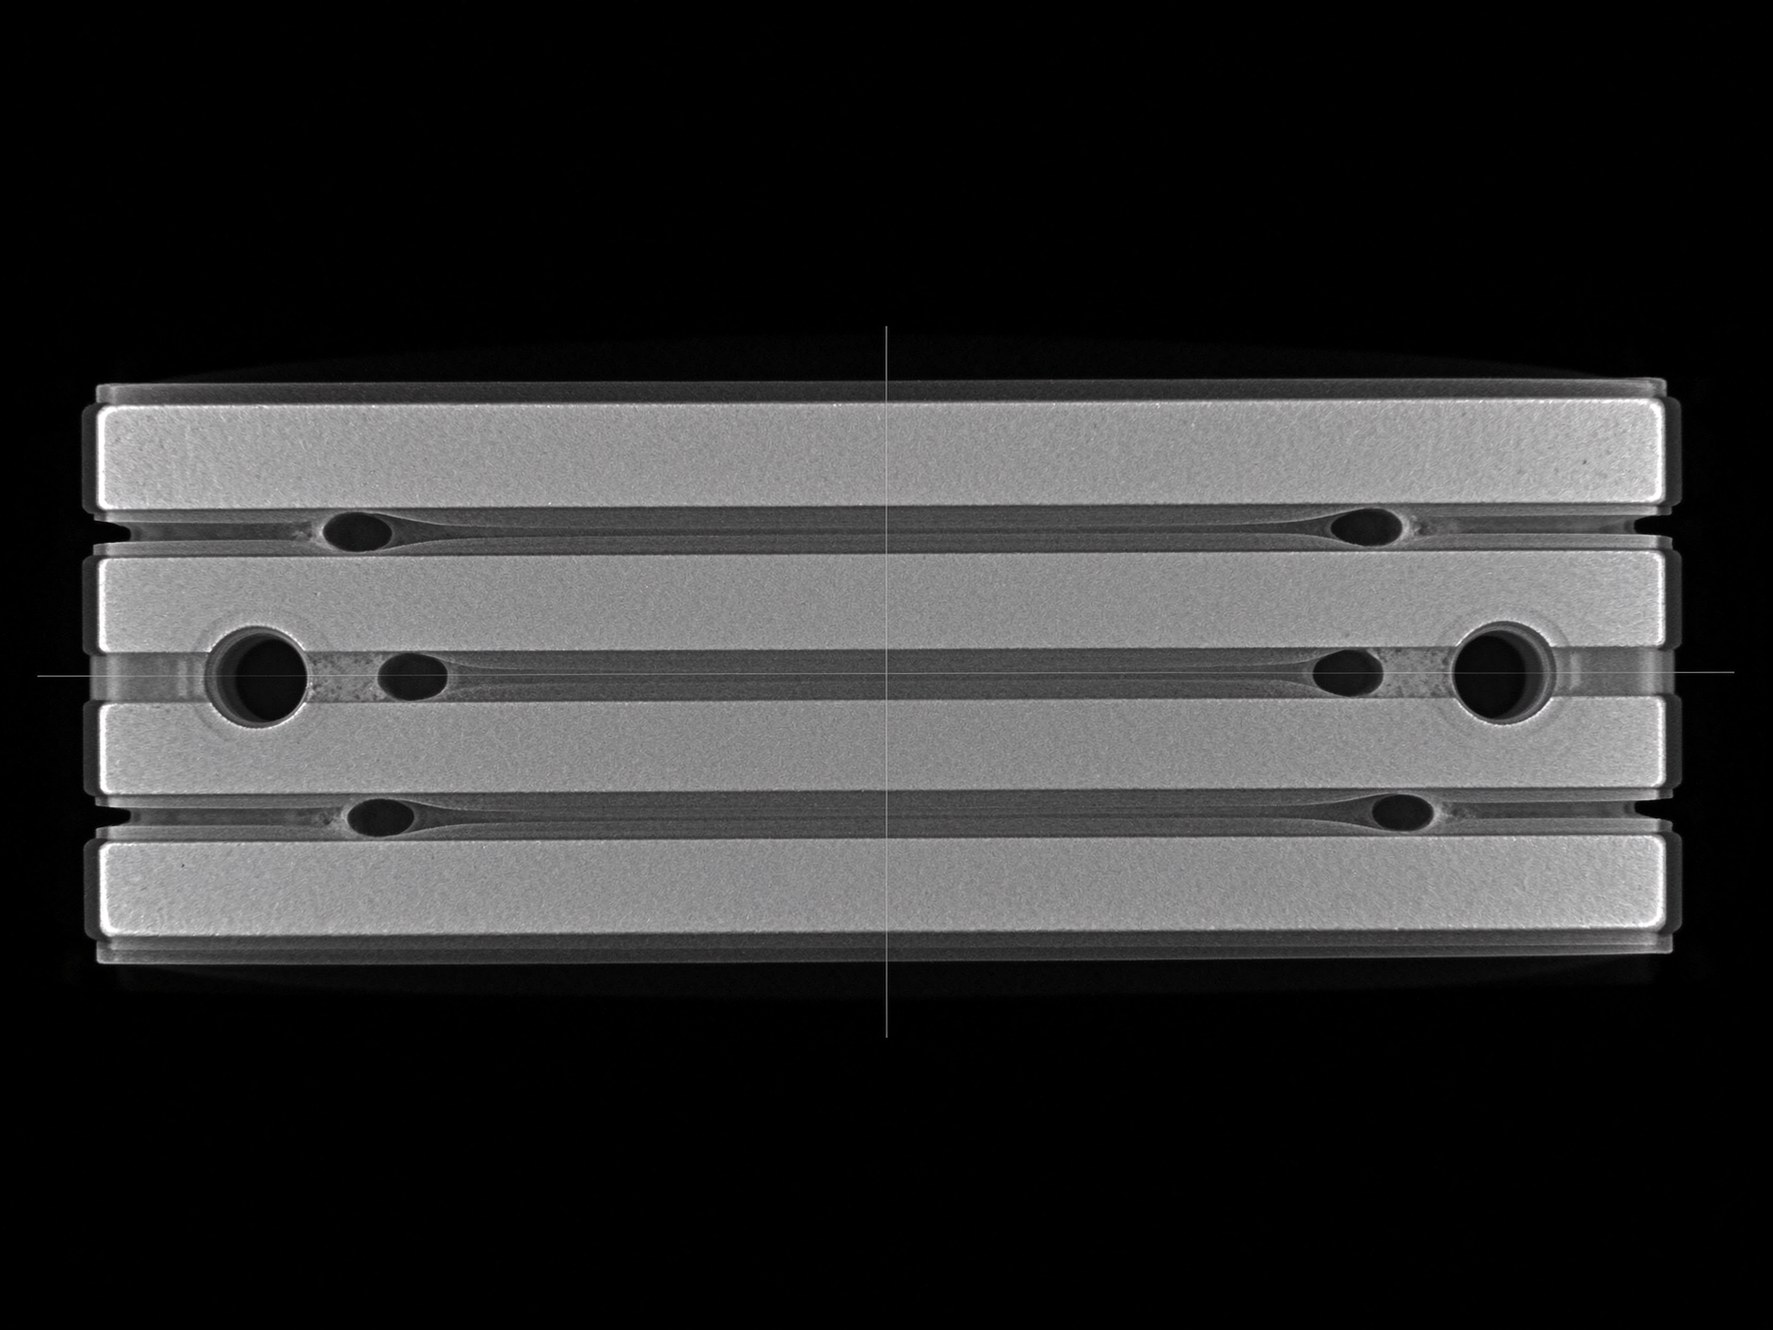
Internal voids do not punch a laminated busbar on day one. They distort the local electric
Read article
Nadia Rahman is a quality and compliance engineer with 9 years in electrical-component quality systems. She manages SHANYUAN's ISO 9001 and IATF 16949 programmes, incoming and outgoing inspection, and UL/IEC compliance documentation. She holds a B.Sc. in Industrial Engineering from the Universi
Send the current profile, voltage class and terminal types — our engineers reply within one business day.
