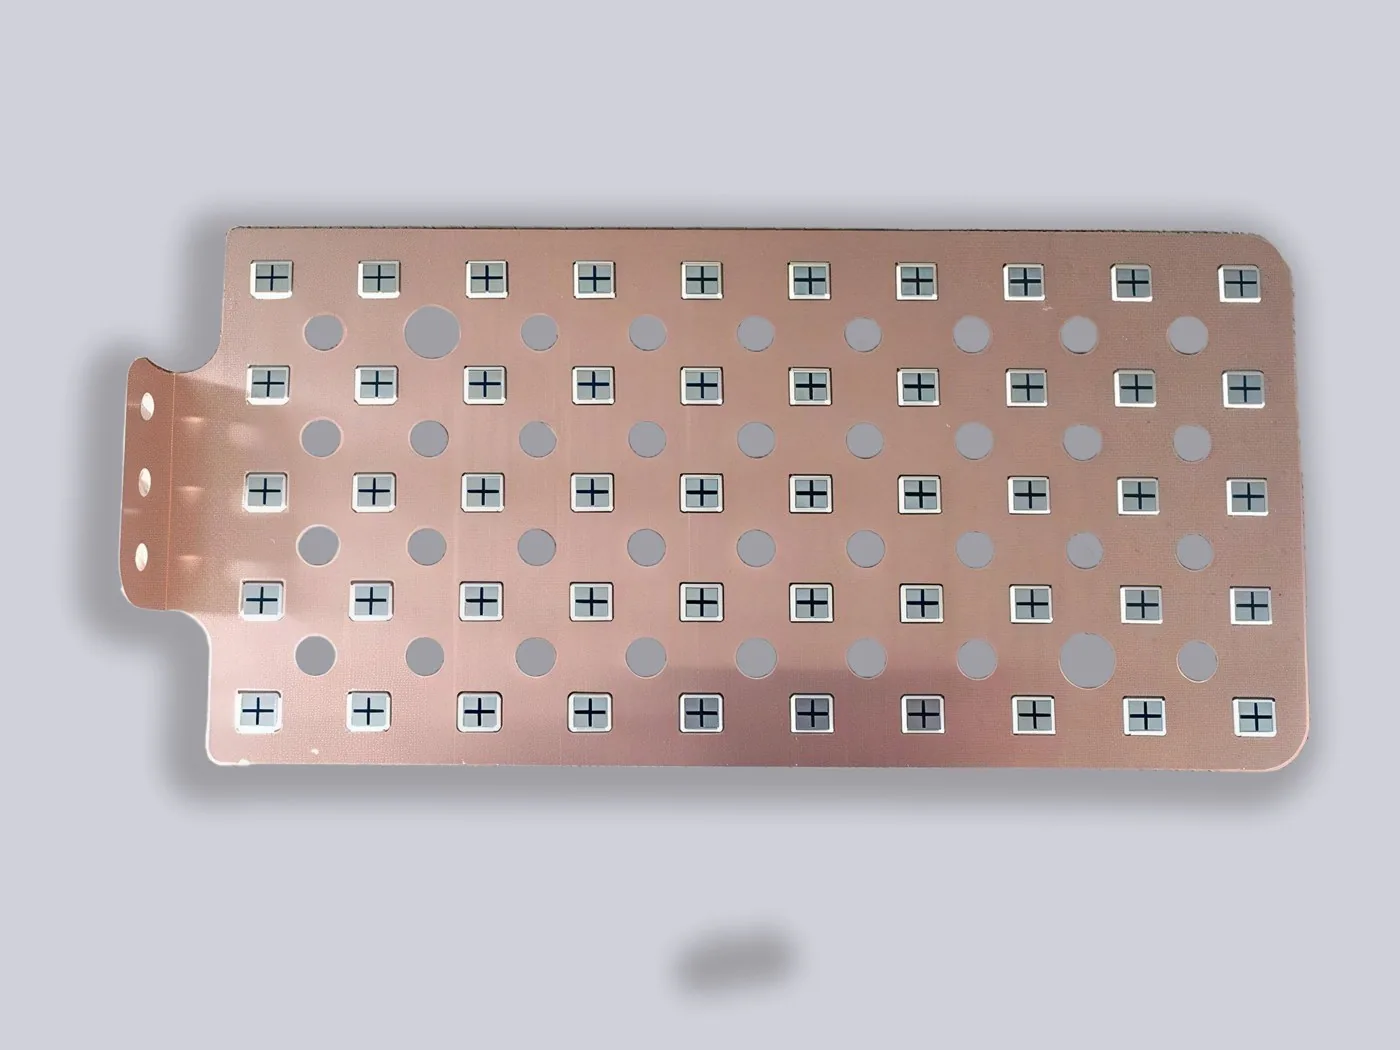
Andino Drives, a Brazilian manufacturer of industrial variable-frequency drives, engaged SHANYUAN in 2026 to replace the cable-based power interconnects in its 400 A VFD cabinet line. The laminated three-phase busbar cut cabinet wiring by 60%, saved two hours of assembly time per unit, and passed the IP20 clearance and creepage tests for the open-frame design.
This case study is published as a representative engineering project. The product photograph and released drawing are illustrative of the delivered part; exact dimensions are covered by the customer's non-disclosure agreement.
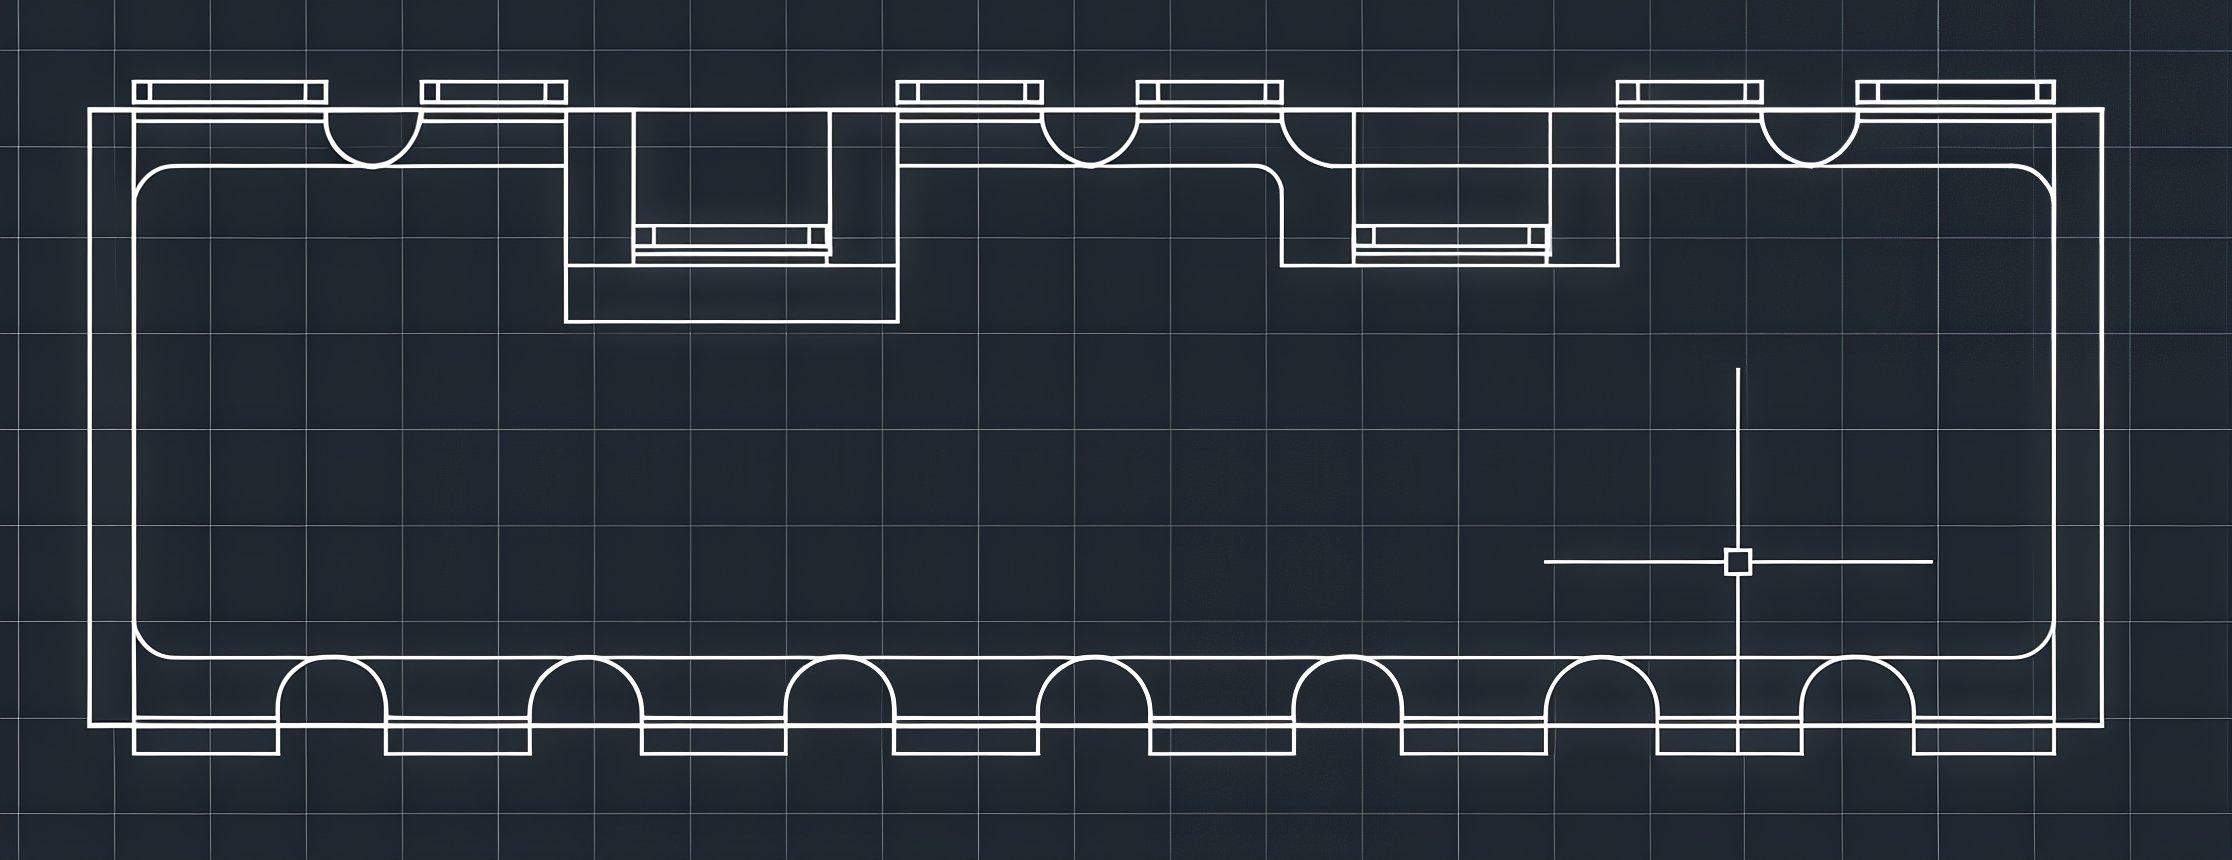
Customer drawings are treated as confidential; excerpts shown here are provided with permission and illustrate the layer stack, terminal layout and dielectric boundaries of the delivered part.
| Customer & platform | Andino Drives 400 A industrial VFD, 480 V three-phase |
|---|---|
| Busbar type | Three-phase laminated busbar, C11000 copper, 2.0 mm conductors |
| Dielectric system | PET film wrap, 2.5 kV hi-pot, IP20 clearance |
| 정격 전류 | 400 A continuous, 500 A 60 s |
| 온도 상승 | ΔT 26 °C at rated current, 45 °C ambient |
| Wiring reduction | 60% less cabinet wiring, 2 h assembly saving per unit |
| Terminals | Bolted taps for module and line/load connections, tin-plated |
| Production | Monthly batches, 100% hi-pot per part |
| Quantified result | 60% less wiring, 26 °C ΔT, 400 A, 2 h saved per unit |
Andino Drives, a Brazilian manufacturer of industrial variable-frequency drives, engaged SHANYUAN in 2026 to replace the cable-based power interconnects in its 400 A VFD cabinet line. The laminated three-phase busbar cut cabinet wiring by 60%, saved two hours of assembly time per unit, and passed the IP20 clearance and creepage tests for the open-frame design.
Andino's 400 A VFD cabinet used individual cable runs between the input terminals, DC-link, IGBT modules and output terminals. Field service data showed that most wiring errors happened during this cable dressing, and the cabinet builder needed roughly 4 hours per unit for routing, lacing and testing the power interconnects.
The customer asked SHANYUAN for a three-phase laminated busbar that would carry the 400 A power path in one part, accept the standard module and terminal connections, and pass IP20 clearance for the open-frame cabinet. The busbar vs cable guide documents exactly this trade-off: impedance, thermal behaviour and assembly cost.
The application matches the industrial application page; our manufacturing process article describes how the one-piece part is produced.
The delivered busbar carries all three phases in a single laminated stack, with insulated inter-phase spacing and bolted taps at the module positions and at line/load ends. Phase-to-phase insulation uses PET film with a 2.5 kV hi-pot rating, giving IP20-class clearance in the open frame.
Module taps use M8 studs with torque stripe; the design reuses the busbar components pattern for the mounting hardware. The complete part installs in 25 minutes versus roughly 3 hours of cable dressing — the 60% wiring reduction the customer recorded on the first production batch.
The layer stack and conductor sizing follow the design guide and the ampacity chart; for the 400 A rating with 60 °C operating temperature the 2.0 mm conductors carry comfortable margin.
Temperature-rise testing at 400 A in a 45 °C ambient chamber measured 26 °C rise with the hot spot at the output tap — inside the 30 °C budget. The thermal management guide documents the cabinet convection assumptions for open-frame VFDs.
Manufacturing uses the standard lamination line: stamping, stacking, vacuum lamination, terminal assembly and hi-pot test. The welding and bending steps follow the welding and joining guide; terminal machining follows the terminal machining guide.
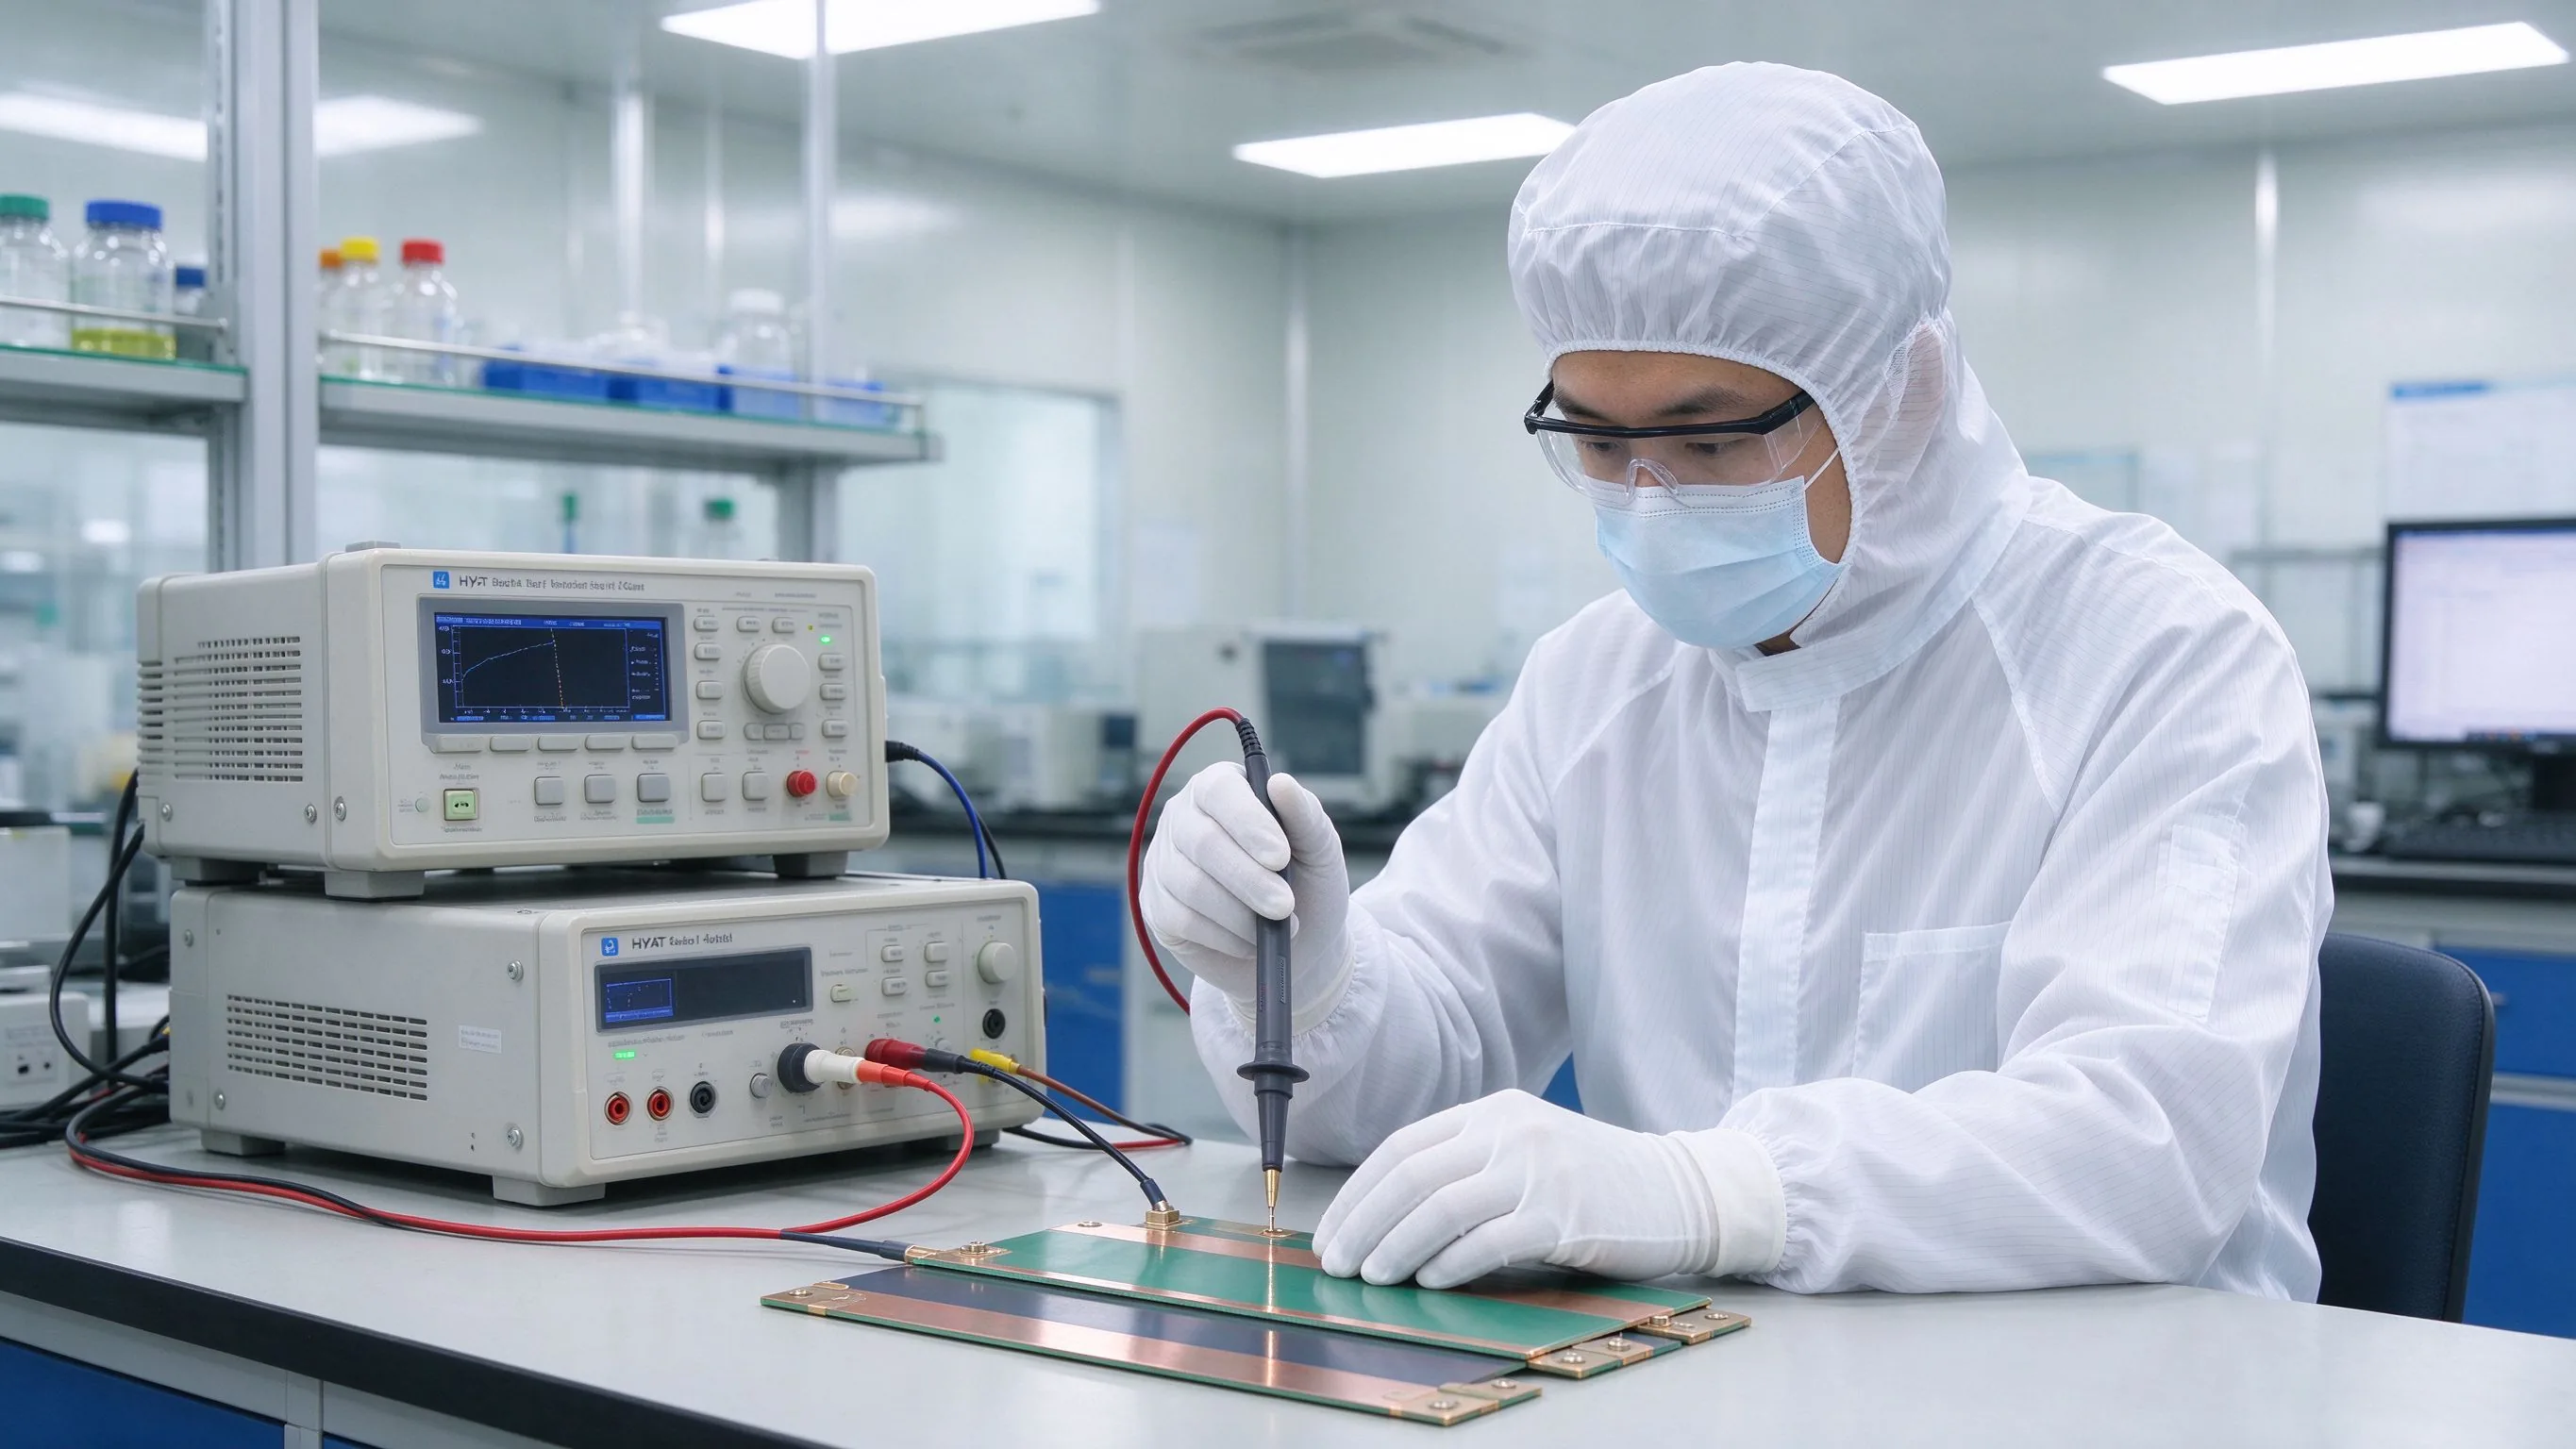
Because the VFD market is cost-sensitive, the design uses standard C11000 copper and PET film — no exotic materials — while keeping joint resistance below 30 μΩ per tap, verified with a four-wire meter.
Qualification covered a 2.5 kV hi-pot, thermal cycling −25 °C to +70 °C, and a 1000-hour loaded endurance run on the prototype cabinet. All passed; the customer's test laboratory verified the thermal-rise and wiring-reduction claims independently.
Series production runs in monthly batches aligned with Andino's cabinet build plan. Every part receives a 100% hi-pot test at the quality laboratory, and each batch ships with a joint-resistance scan record. The factory tour shows the production stations.
The customer's assembly line now installs the busbar in 25 minutes with a single torque-audit step, and rework from wiring errors dropped to near zero on the first three production months.
The delivered busbar met every target: 400 A continuous with 26 °C rise, 60% less cabinet wiring, two hours of assembly time saved per unit, and IP20-clearance pass in the open-frame cabinet.
Across Andino's 4000-unit annual build, the assembly saving is roughly 8000 labour-hours per year, and the single-part BOM simplified their inventory: one busbar SKU replaced ten cable SKUs. The automated production article and the DFM checklist explain why the one-piece approach scaled so cleanly.
For VFD and industrial drive engineers, the industrial application page, the power electronics busbar range and the engineering contact form are the entry points we recommend.
Thomas O'Brien은 적층 버스바의 스탬핑, 적층, 단자 가공에 14년 경력을 가진 제조 공정 엔지니어입니다. 정밀 절단 프로파일, 절연층, CNC 단자 가공 생산 라인을 관리하며 치수 제어와 대량 생산 재현성에 주력합니다. TU Dublin에서 기계공학 디플로마를 취득했습니다. 버스바 제조와 자동화 생산 라인에 대해 집필합니다.