月~金 9:00–18:00 · 中国標準時(UTC+8)· 山東省・中国
Quality & Testing

Built, Inspected and Documented

Laminated busbar quality is determined long before the first electrical test — it is built into the layup, the lamination window and the terminal welding.

Manufacturing Process

Eight controlled steps from copper sheet to tested part

Material PreparationCopper (C11000) or aluminum inspected for thickness tolerance
Punching & Laser CuttingConductor profiles, holes and windows cut to drawing
Surface FinishingTin plating for corrosion resistance and joint solderability
Dielectric LayupPET, Nomex or epoxy films by voltage class
LaminationHeat and pressure held to recipe; dielectric thickness in tolerance
Edge SealingExposed dielectric layers cannot creep or arc
Terminal AssemblyStuds, blade tabs and fused links welded in position
CNC Trim & InspectionFinal dimensional verification against the released drawing
入荷材料

積層に入るもの

MaterialStandard options
ConductorsC11000 copper as standard; aluminum available on request
DielectricsPET, Nomex and epoxy (DLF) films, selected by voltage class and operating temperature
PlatingTin finish for corrosion protection and joint solderability
13+2012年からの実績年数
1–6+導体層数
~1000 A定格電流
1 day技術回答
試験と検査

すべての生産ロットを梱包前に検証

Dielectric Withstand (Hipot)

Per customer specification and applicable standard.

Insulation Resistance

Measured on sampled parts per lot.

Dimensional Inspection

Terminal positions, hole sizes and envelope vs drawing.

Visual Inspection

Plating coverage, edge sealing and weld quality.

Continuity Check

Electrical verification of each conductor path.

文書化

監査可能な記録

寸法・電気試験記録は生産ロットごとに管理され、要求に応じて出荷に添付できます。
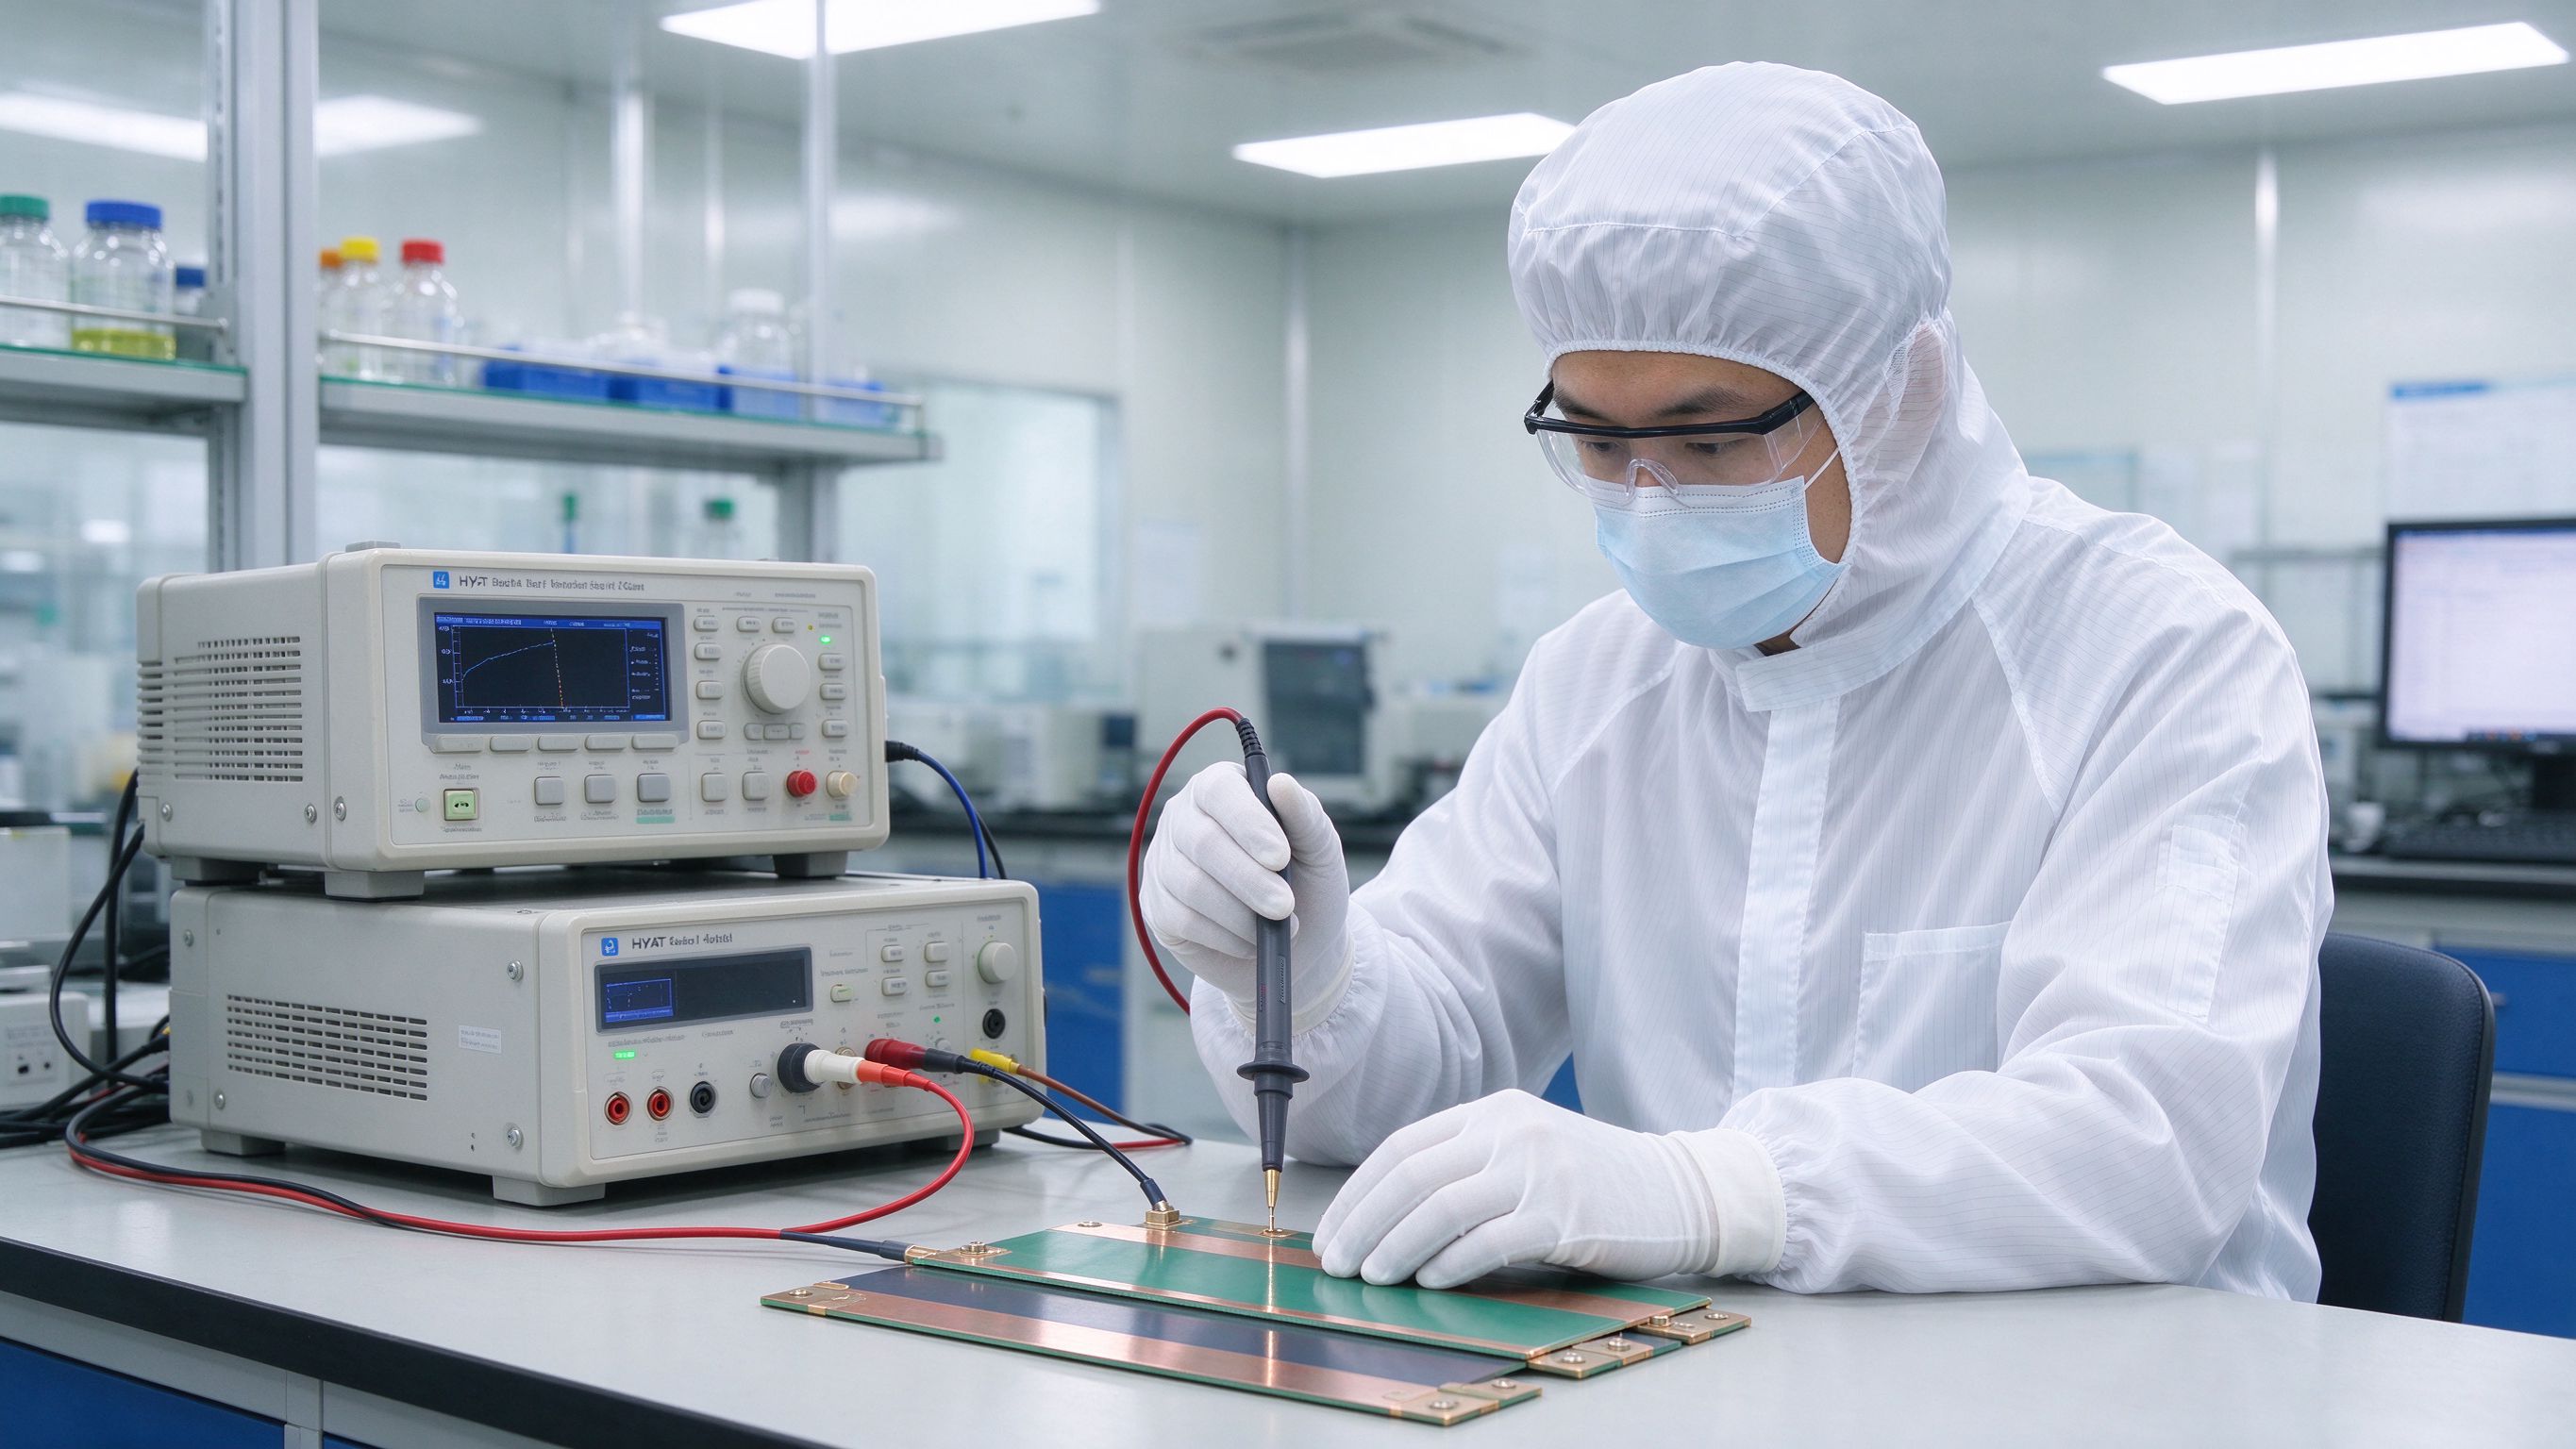
  • Batch test records per production lot
  • Certificates of Conformance (CoC) on request
  • PPAP-style documentation aligned at quotation
  • Test records aligned with your quality system
Inspection and test bench
製造性のための設計

早期発見、安価な修正

金型が切られる前に、当社エンジニアが図面のDFMレビューを実施します – 層数、電流経路、端子間隔、端部距離、誘電体クリアランス。この段階で端部距離の不足や溶接ゾーンの過小設計を発見する方が、生産中に見つけるよりはるかに安上がりです。

01

Layer count

Stack-up validated against voltage class and current.

02

Current paths

Cross-sections checked against continuous and peak current.

03

Terminal spacing

Pitch and weld zones matched to mating hardware.

04

Edge distances

Creepage and dielectric clearances verified before tooling.

Standards Our Customers Reference: How They Shape the Design

Our in-house QC process — hipot, insulation resistance, dimensional, visual and continuity checks on every lot — is the internal half of quality. The external half is the standards landscape our customers design to, and it is worth being explicit about which standards apply to power-interconnect parts and how they show up in the drawings we build to.

POWER DISTRIBUTION
UL 1977

Component assemblies used in power distribution, including high-current connectors.

CANADIAN COUNTERPART
CSA C22.2 No. 182.3

Sits alongside UL 1977 on recognized connectorized power-distribution assemblies.

FLAMMABILITY
UL 94 V-0

Routine expectation for insulator housings and dielectric systems on shipped parts.

ENVIRONMENTAL
RoHS / REACH

Baseline on shipped product; halogen-free constructions available where the spec calls for it.

Application-level standards: SAE J1772 · EV charging couplersOpen-rack platform specs · in-rack busbar interfaces — these set the current-interruption, arcing and cycle-life tests the interconnect must pass.
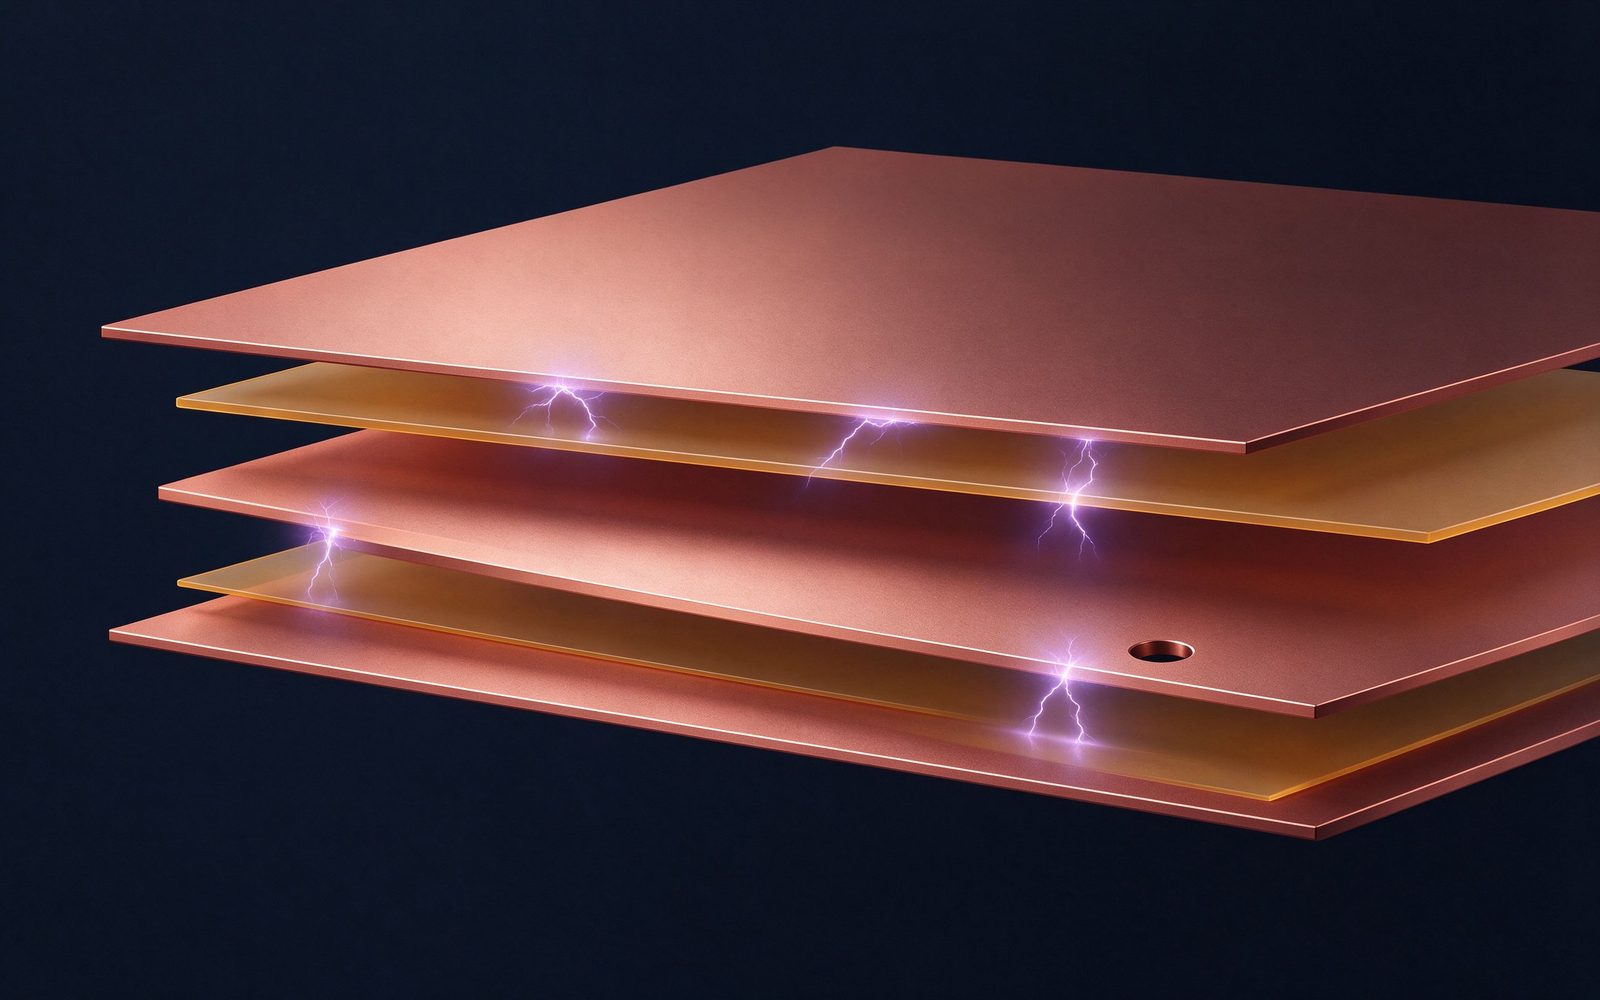
Partial discharge cutaway of a laminated busbar edge seal

What this means for a laminated busbar

  • Creepage & clearance follow the voltage class implied by the referenced standard.
  • Edge sealing & dielectric selection are driven by the partial-discharge expectations of the test specification.
  • Terminals & contact lands are sized against the standard’s temperature-rise and hot-swap requirements.

We do not hold aerospace or defense qualifications ourselves — and we do not claim to — but customers in those programs routinely flow down their own standards and special-process requirements to the parts we build.

These standards are frequently referenced by our customers. We build to the drawing and test specification provided, and every released batch ships with its own hipot, insulation-resistance and continuity records.

Two technical references explain the physics behind the tests we run:

品質への約束

ロット単位で文書化

品質は積層、ラミネーション条件、端子溶接に組み込まれ、その後検証され記録されます。

製治具着手前にDFMレビューを実施生産ロットごとに社内QC検査ご要望に応じてロット試験記録を提出CoC/PPAP形式の品質文書に対応
技術資料

さらに深く

積層バスバー設計ガイド

構造、誘電体選定、通電容量の基礎。

設計ガイドを読む

バスバー許容電流チャート

ディレーティング指針付き銅定格電流。

銅チャートを見る

バスバー vs ケーブル

積層が勝つ場面と勝たない場面。

バスバーとケーブルを比較

Documented, batch by batch.

Dimensional and electrical test records per lot — CoC and PPAP-style documentation aligned at quotation.

FAQ

よくある質問

エンジニアリングチームによる明確な回答。

量産ロットではどのような試験を行いますか?
試験は設計確定時に合意した仕様に沿って行います:絶縁耐力試験(hipot)、絶縁抵抗、寸法検査、めっきと端面シールの外観検査、導体経路ごとの導通確認です。
品質システム向けの文書は発行できますか?
寸法・電気試験記録をロットごとに保管しています。CoC、指定フォーマット、PPAP形式の文書が品質システムで必要な場合は、見積り段階でお知らせください。要求に合わせて書類を整えます。
量産前の小ロット試作に対応していますか?
はい。カスタム案件は通常、仕様レビュー→DFM→見積り→はめあい・電気的検証用サンプル製作→ロットごとのQC記録付き量産、の流れで進めます。
図面はどのファイル形式に対応していますか?
PDF、DXF、STEP に加え、既存部品の写真も受け付けます。見積りには寸法・公差を記載した2D図面で十分です。3DモデルがあればDFMレビューと製治具準備が速くなります。
バスバーに保証はありますか?
はい。購買契約に記載した保証期間内は、材料および製造上の欠陥を保証します。不適合部品は手直しまたは交換し、ご要望に応じて不良解析を共有します。
国際配送と梱包に対応していますか?
はい。端部保護、帯電防止フィルム、輸出用カートンを用い、ご指定の荷扱い条件で梱包し、海上または航空便で発送します。都度、インボイス、梱包明細、試験記録などの商務書類を添付します。

Need test records with your shipment?

Tell us at quotation stage — we align CoCs, PPAP-style documentation and test records with your quality system.
